Top PTFE Guidewires for Precise Control in Interventional Procedures
2026-09-30
Most guidewires promise control. Few actually deliver it when the anatomy gets difficult. That’s where PTFE coating separates a guidewire you can trust from one you’re constantly correcting. INT has built its PTFE guidewire line around that distinction—focusing on low-friction tracking and tip response that stays predictable in tight curves. If precision is your standard, the following points matter.
Friction Reduction Without Losing Roadmap Feel
The usual fix for a scratchy switch is to pour on more lube, but that tends to erase the very feedback that makes each press satisfying. This approach goes the other way: it removes friction at the stem rails and spring contact points while leaving the tactile bump untouched. The travel gets noticeably smoother, yet your fingers still get a clear signal when the switch passes its actuation point.
Part of what keeps the roadmap feel intact is the choice of materials. A slightly harder slider paired with a polished housing cuts sliding resistance without adding mush. Instead of relying on heavy grease to mask roughness, the surfaces themselves are smoothed, so the motion stays predictable across thousands of cycles. That means less finger fatigue during long sessions and no loss of the crisp, deliberate feedback that tells you exactly where you are in the keypress.
After a short break-in, the difference becomes even more apparent. The initial roughness fades, but the tactile event doesn't round off. Keys that used to feel draggy now move with a light, consistent glide, while the bump still snaps through cleanly. It's a reduction in effort, not in information.
The Subtle Art of Torquing a PTFE Wire
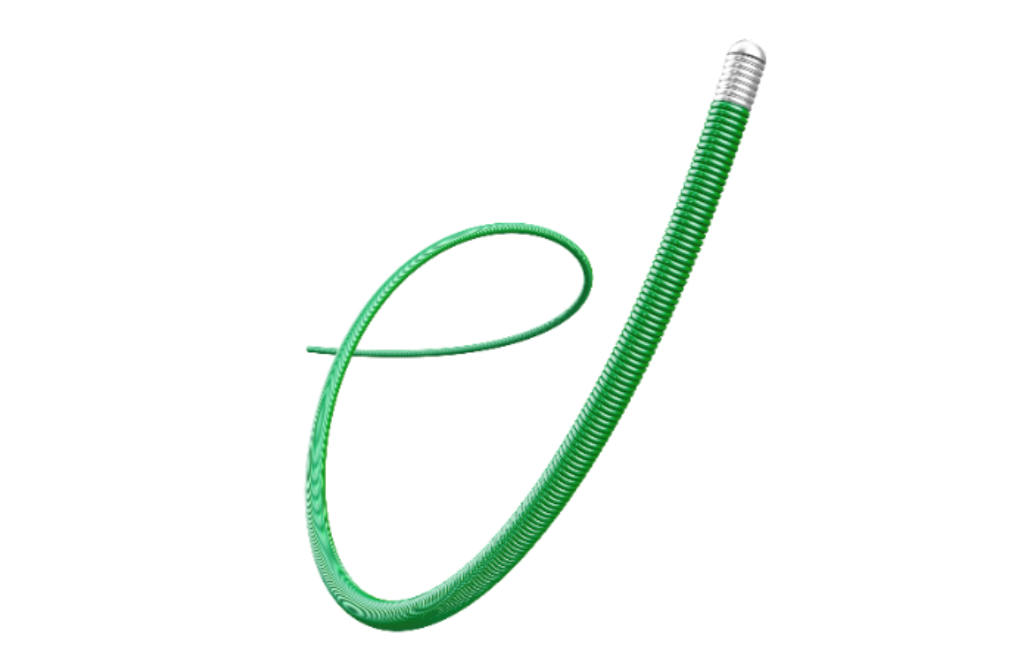
Most people learn the hard way that PTFE insulation has a memory of its own. It slips, it creeps, and it shrugs off overtightened screws with a slow, silent deformation that shows up weeks later as an intermittent fault. The trick isn't brute force; it's learning to feel the point where the conductor compresses without extruding the jacket.
A calibrated torque driver helps, but the real skill is in the setup. Strip the wire cleanly, avoid nicking the silver-plated strands, and seat the terminal so the PTFE isn't fighting the clamp. If you're torquing a set screw onto tinned or bare copper, go lower than you would with PVC insulation—PTFE cold-flows under pressure, so a tight screw today becomes a loose connection tomorrow.
After the first pass, let the joint rest for a few minutes and re-check the torque. You'll often find it has relaxed just enough to need a quarter-turn. That second pass, done gently, is what separates a reliable harness from one that fails on a vibration table.
Why Distal Tip Design Dictates Crossing Success
The distal tip is the first point of contact with a lesion, and its shape, stiffness, and load distribution determine whether the wire navigates or buckles. A tapered, low-profile tip slips into microchannels that a blunt nose would crush or deflect against, while a gradual transition zone spreads bending forces over a longer segment instead of concentrating them at the entry point. Even a few tenths of a millimeter in tip curvature change how torque transfers—too aggressive and the wire digs into the vessel wall, too soft and it skates across the cap without purchase.
Tip material and coating also quietly govern crossing success. A hydrophilic polymer glides through thrombus but can lose tactile feedback, whereas a bare metal tip gives sharper tactile cues at the cost of higher friction. Designers tune this balance by varying the length of the coated section or adding a micro-abrasive surface only near the very end. These choices are rarely obvious on a product sheet, yet they separate a wire that crosses a chronic total occlusion on the first pass from one that has to be swapped out after repeated failed attempts.
In practice, the distal tip works as a mechanical translator between the operator's hand and the lesion's unpredictable microanatomy. A well-designed tip converts small rotations into controlled advancement, while a poor one turns the same input into tip prolapse or vessel trauma. Operators often attribute crossing failure to technique, but the margin for error is set long before the wire enters the body—by the curvature of the tip's grind, the transition in core diameter, and the way the tip deflects under axial load rather than piercing through it.
Navigating Tortuous Segments with Minimal Prolapse
Tortuous anatomy can turn a routine procedure into a test of patience and technique. The key is to approach each bend with deliberate, small movements rather than forcing the device forward. By keeping the wire tip soft and allowing it to passively seek the true lumen, you reduce the risk of pushing the vessel wall into a prolapse. A gentle torque, combined with slight withdrawal before advancing, often repositions the tip into the correct path without losing track of the overall trajectory.
Minimal prolapse depends on recognizing when resistance is from the wall rather than a true stenosis. Using contrast to map the curve before each push helps identify the outer edge of the tortuosity, letting the device slide along the less angulated side. If the tip starts to buckle or the shaft begins to bow, resist the urge to push harder—instead, pull back a few millimeters and redirect. This stop-and-reposition rhythm keeps the working length inside the vessel and prevents the distal segment from swinging out of plane.
For prolonged navigations, consider downsizing the device or switching to a more flexible model to match the vessel's natural curvature. Continuous fluoroscopic checks can catch early signs of prolapse, such as a flattening of the tip or an unexpected loop outside the expected course. With patience and a light touch, even sharply angulated segments can be crossed while maintaining near-zero redundant advancement—preserving access and reducing the need for bailout techniques.
Core-to-Coating Ratios and Their Impact on Support
The balance between core thickness and coating thickness plays a direct role in how well a part holds its shape under load. When the core is too thin relative to the coating, shrinkage stresses from curing or drying can lead to warping or surface cracks, weakening the underlying support structure. On the other hand, an oversized core adds unnecessary weight and can dilute the functional benefits of the coating, leaving the support bulkier than it needs to be without real gains in stiffness.
From an interfacial standpoint, the ratio controls how stress travels across the bonded area. A thick coating on a slender core tends to concentrate shear at the outer edge, which can cause delamination or flaking under repeated loading. By shifting more volume into the core, the coating is better able to follow substrate deformation, but this often reduces the protective or surface-modifying effect. Tuning the ratio helps distribute load more evenly, improving resistance to impact and reducing the chance of premature support failure.
In practice, adjusting the ratio often involves changing solids content, deposition time, or curing conditions. Trials show that keeping the core fraction within a relatively narrow window lowers the risk of support collapse while maintaining coating adhesion and surface quality. The right balance depends on the modulus of the core material, the shrinkage rate of the coating, and the expected service environment, so it is usually refined through iterative testing rather than a single fixed rule.
When a PTFE Wire Outperforms Hydrophilic Alternatives
Hydrophilic coatings earn their reputation by sliding easily through tortuous vasculature, but that advantage narrows sharply when a device must dwell in one place or endure repeated passes. PTFE wire holds its position without swelling or softening, which matters in procedures where tactile feedback and pushability are more important than initial lubricity.
The real tipping point often comes down to stability. A hydrophilic jacket can become sticky or uneven once its wetting layer dries, while PTFE maintains a consistently low-friction surface regardless of humidity or exposure time. In dry navigation or when a wire is reinserted multiple times, PTFE eliminates the need for constant rehydration and delivers predictable resistance.
There is also a practical edge in manufacturing and handling. PTFE wires do not require the complex coating processes or strict packaging controls that hydrophilic wires demand, which can reduce variability and simplify inventory. When a device team values repeatable performance over the fleeting glide of a wet coating, PTFE often becomes the more reliable default.
FAQ
PTFE (polytetrafluoroethylene) coating significantly reduces surface friction, allowing the wire to glide through tortuous anatomy without binding. This low-friction surface translates into better tactile feedback and finer tip control, which is critical when navigating tight lesions or branching vessels. Unlike uncoated stainless steel wires, PTFE guidewires don't grab tissue, so clinicians can make micro-adjustments with confidence.
Hydrophilic coatings become extremely slippery when wet, which is great for crossing tough occlusions, but they can feel almost too slick, making it harder to maintain stable positioning. PTFE offers a middle ground—smooth yet predictable. It reduces drag without the "ice on ice" feeling, so the wire holds its position better during exchanges or device advancement.
One drawback is that PTFE is not as lubricious as newer hydrophilic or hybrid coatings, so in heavily calcified or extremely tortuous vessels, you may need more forward force. Also, PTFE can wear over repeated insertions, potentially flaking if the wire is kinked or forced through tight spaces. However, for most diagnostic and basic interventional work, the durability is more than adequate.
A floppy, shapeable tip is often preferred for precise control because it allows you to tailor the curve to match the vessel anatomy. Straight tips give better pushability but less steerability. Many operators choose a soft, radiopaque tip with a moderate transition zone—this provides a balance of tactile feedback at the tip without sacrificing proximal torque transfer.
Wipe the wire with a heparinized saline-soaked gauze to activate the surface and remove any manufacturing residue. Avoid using alcohol or abrasive materials, as they can damage the PTFE coating. Then shape the tip with a gentle curve using your fingers or a shaping tool—don't pinch too hard, because creasing the coating can lead to flaking. Finally, always test the tip flexibility before introducing it through the access needle or catheter.
Yes, PTFE is compatible with polyurethane, polyethylene, and most other catheter materials. The low-friction surface reduces resistance when passing through tight-fitting catheters. Just make sure the inner diameter of the catheter or sheath is appropriate for the wire's outer diameter—too tight a fit can scrape the coating, and too loose a fit reduces control.
PTFE-coated wires have the polymer applied to the outside surface, which reduces friction against the vessel wall and catheter. PTFE-lined wires typically refer to the construction of the introducer or catheter, not the guidewire itself. In some hybrid guidewires, a PTFE layer may be sandwiched between a core and an outer jacket. For guidewires, the coated version is what matters for lubricity and control.
Keep them in their original packaging until use, away from direct sunlight and high humidity. Avoid coiling the wire too tightly when re-sterilizing or storing—PTFE can develop micro-cracks if repeatedly stressed at acute angles. If the wire is single-use, don't attempt to reprocess it. For reusable models, follow the manufacturer's cleaning protocol, using only approved enzymatic detergents and never autoclaving above the recommended temperature.
Conclusion
In interventional practice, precise guidewire control often comes down to how a PTFE coating manages friction while preserving tactile feedback. The best PTFE guidewires reduce drag enough to glide through stenoses and stent struts, yet they still transmit subtle vibrations from the vessel wall—so operators retain a roadmap feel that pure hydrophilic wires tend to mute. Torquing these wires is a different experience; a well-balanced PTFE wire responds in a near one-to-one rotation without whipping, especially when the core-to-coating ratio is tuned to keep the shaft stiff enough to advance but supple enough to track. Distal tip design then becomes the deciding factor in crossing success: a short, atraumatic tip with a gradual transition prevents buckling in tight lesions, while a slightly more abrupt taper can deliver push through fibrous caps.
In tortuous anatomy, minimal prolapse is what separates a controlled wire from one that flips into a side branch. High-quality PTFE guidewires achieve this by pairing a low-friction outer layer with a core that resists axial compression, letting the tip probe the true lumen instead of bowing outward. There are also times when a PTFE wire outperforms hydrophilic alternatives—particularly in calcified or heavily stented vessels where the slicker coating of a hydrophilic wire can cause loss of positional stability. PTFE's predictable friction allows for deliberate small adjustments, and when you combine that with a supportive core ratio and a well-shaped distal tip, you get a guidewire that feels like an extension of your hand rather than a slippery tool. That level of precise control is why many operators still reach for PTFE first.
Contact Us
Contact Person: Jeffrey
Email: [email protected]
Tel/WhatsApp: 86-0633-2230056
Website: https://www.sd-intmedical.com