Top 10 Roto Moulding Machine Selections That Deliver Superior Performance
2026-09-11
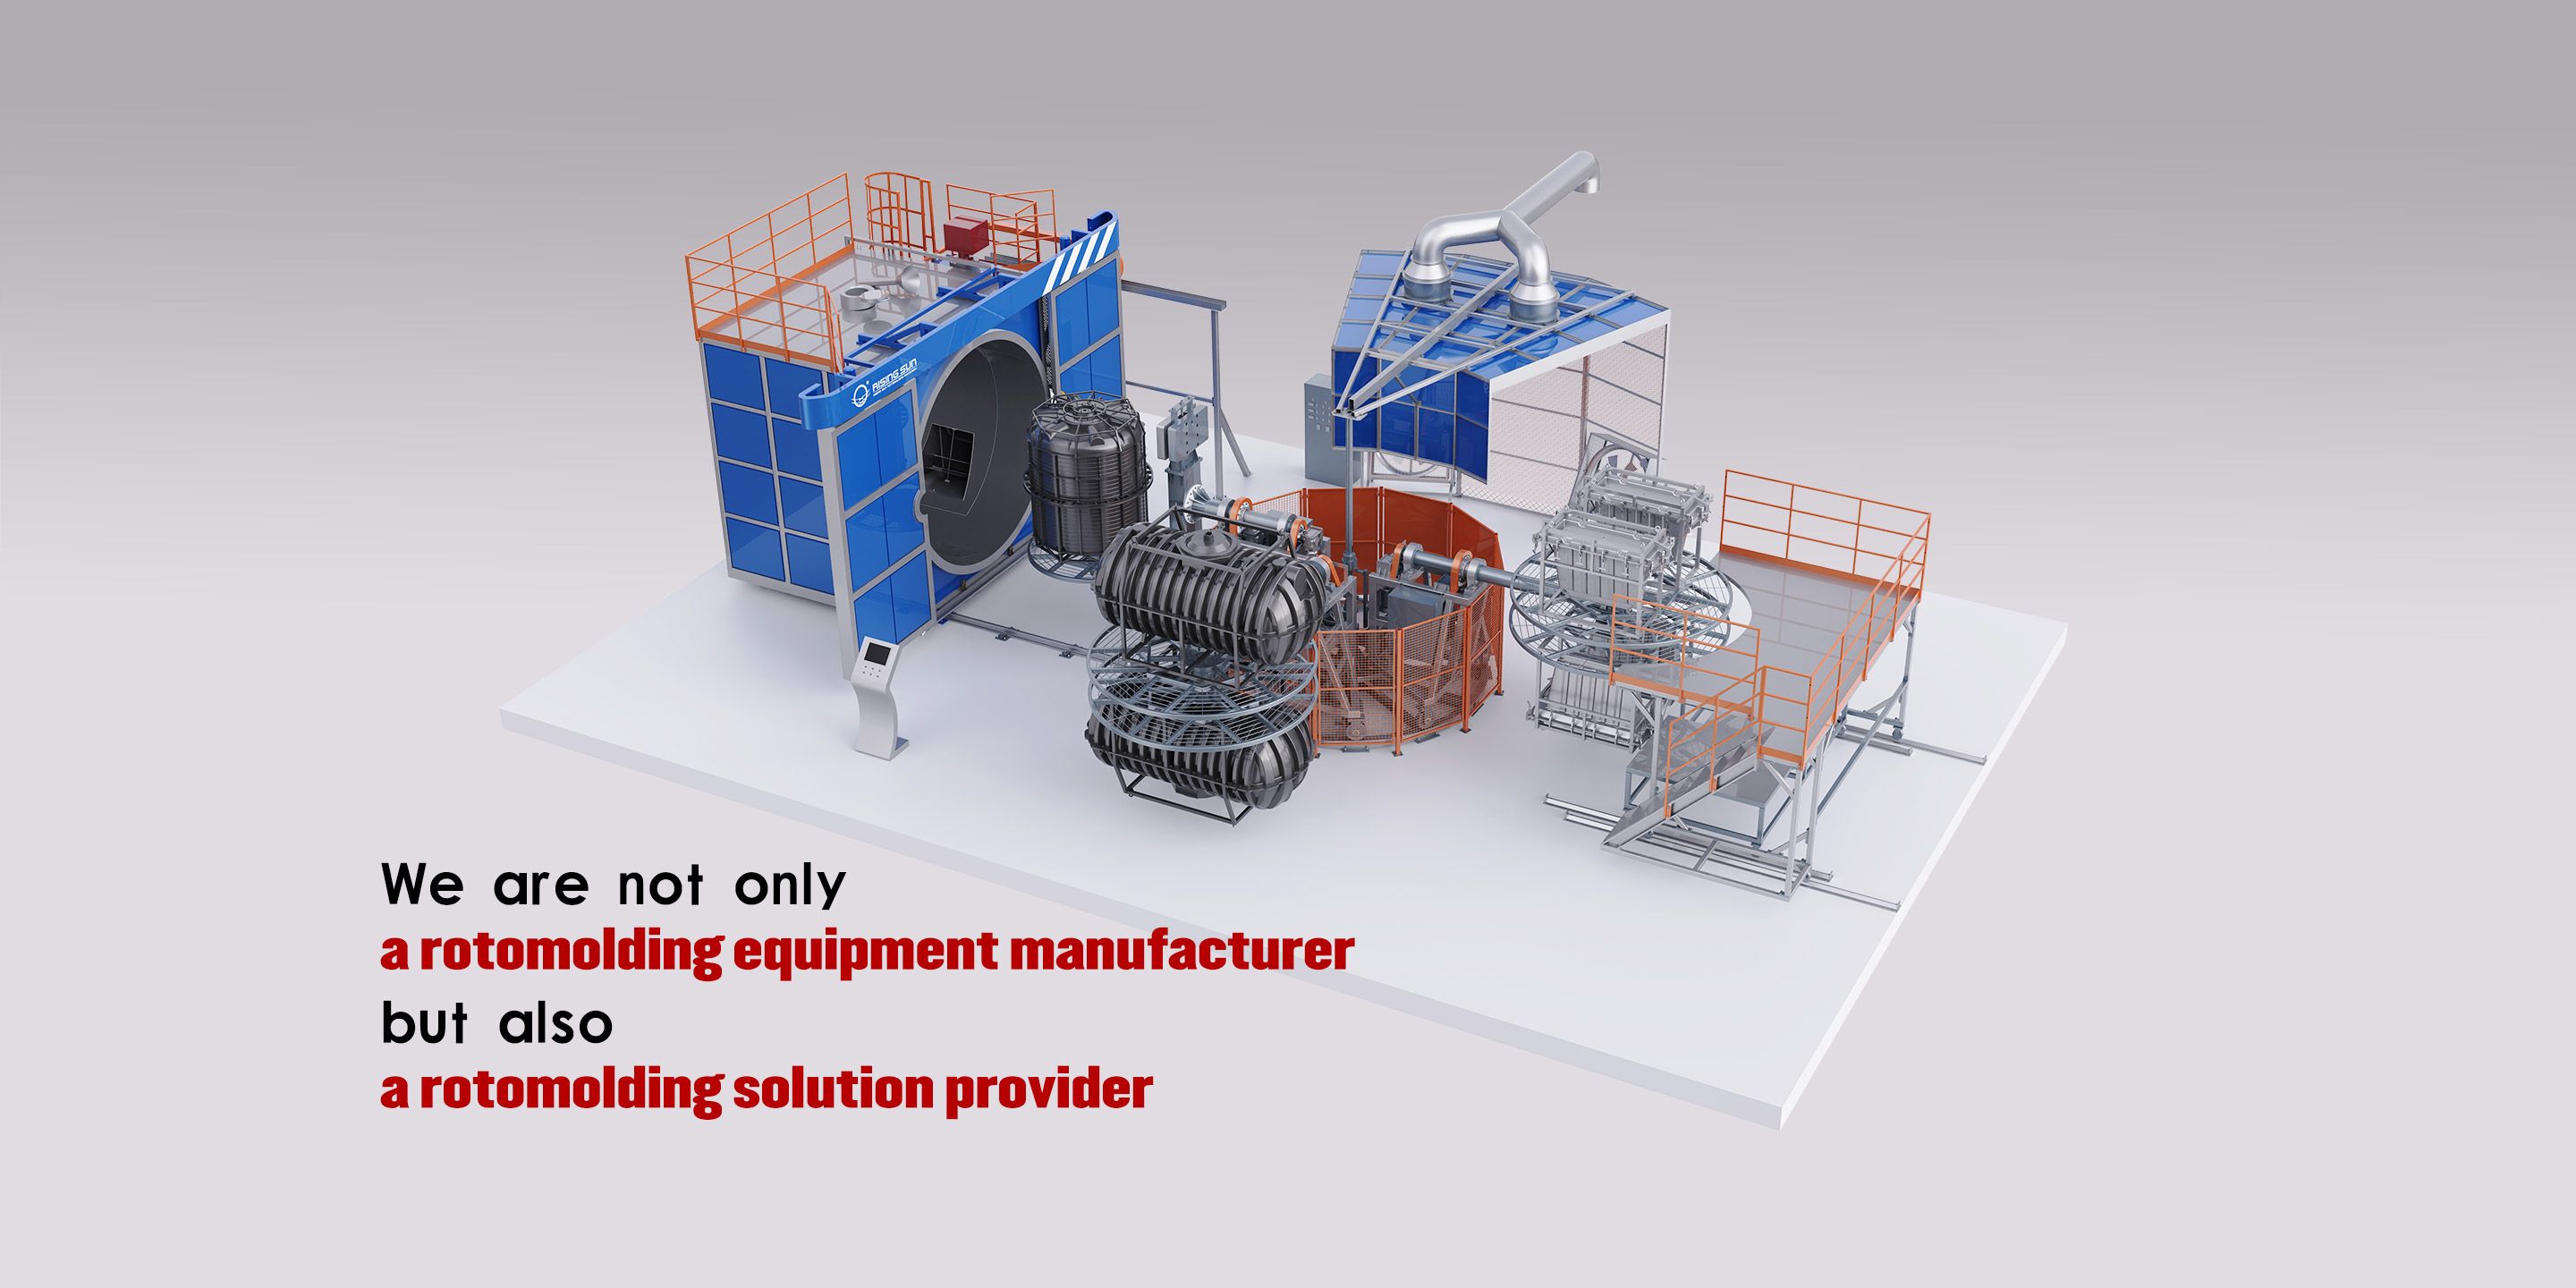
Finding a rotational moulding machine that doesn't just meet specs but actually holds up under daily production pressure is harder than most buyers expect. That's why we've narrowed the field to ten standout options—each evaluated for cycle consistency, energy draw, and long-term reliability. Among them, Rising Sun keeps surfacing as a name worth watching, especially for operations trying to scale without sacrificing finish quality. Here's what separates the best from the rest.
How Build Quality Influences Long-Term Moulding Accuracy
Build quality shapes long-term moulding accuracy in ways that often go unnoticed until production volumes climb. A well-built mould starts with material selection: hardened tool steels that resist wear, combined with precise heat treatment to minimise distortion over time. When cavity dimensions are machined to exacting tolerances and then verified with coordinate measuring equipment, the tool holds its geometry far beyond the initial trial runs. Cheaper alternatives may pass a first article inspection, but microscopic variations in surface finish or uneven hardness create slow drift—flash begins to appear, part weights shift, and dimensional rejects creep upward without a single visible defect in the tool itself.
Rigidity and thermal management are equally critical. A mould base with insufficient plate thickness or poorly fitted interlocks flexes under injection pressure, opening small gaps that lead to flashing and inconsistent packing. Over hundreds of thousands of cycles, this flexing accelerates wear on shut-offs and cores. Conversely, a robust build integrates conformal cooling channels or at least balanced water lines that keep temperatures uniform across the cavity. Without this, hot spots cause localised expansion and contraction that no amount of process tweaking can fully compensate for, especially in tight-tolerance features like thin walls or living hinges.
Finally, the way components are assembled and maintained determines whether accuracy lasts. Dowel pins that are press-fitted with the correct interference, ejector systems aligned to avoid side loading, and accessible wear plates all reduce the gradual loosening that introduces play. In a poorly built mould, maintenance becomes a constant battle: ejector pins bend, slides stick, and parting lines wear unevenly. In a carefully built one, the tool can run for years with only routine cleaning and lubrication, because every mating surface was designed to stay put under real production conditions.
Heating and Cooling Cycle Tweaks That Improve Output
Ramping the temperature up in smaller steps before the main heating phase often does more for consistency than simply extending the soak time. It gives the material a chance to release internal stress gradually, especially in thicker sections where the core lags behind the surface. Instead of jumping straight to the target, try adding a short hold at roughly 60% of the peak temperature. This small pause can reduce warping and prevent micro-cracks from forming later.
The cooling side is where many setups lose more output than expected. Dropping the temperature too quickly after the peak creates uneven contraction, which shows up as distortion or weak spots near joints and edges. A controlled cool-down with an intermediate plateau—often around 30–40% of the peak value—lets the material settle before it reaches room temperature. Even a 20-minute rest at that midpoint can make a measurable difference in dimensional stability.
Adjusting cycle counts is another low-cost tweak that gets overlooked. One extra thermal cycle with a slightly lower peak temperature can refine grain structure and relieve residual stress more effectively than a single long dwell at high heat. Keep the ramp rates modest on the second cycle, and don't rush the final cool. The improvement in throughput often surprises people because the total time barely changes, but the rejection rate drops noticeably.
Single-Arm and Multi-Arm Machines Compared
The choice between a single-arm and a multi-arm machine often comes down to how you want your body to compensate during a set. A single-arm setup forces each side to work independently, exposing strength imbalances you might hide on a bilateral machine. You'll notice the weaker arm fighting for control, the torso twisting slightly to help, and the stabilizers around the shoulder waking up in ways a fixed two-handled path never demands.
Multi-arm machines, by contrast, are built for volume and convenience. Both limbs move together on a linked or mirrored resistance path, which lets you push heavier loads without worrying about drifting off course. That predictability is useful for high-rep burnout sets or when you're short on time, but it also means the dominant side can quietly take over. Many lifters plateau because the stronger arm masks the weaker one over months of bilateral pressing and pulling.
A practical approach is to keep both in your rotation. Use multi-arm machines to build overall mass and work capacity, then switch to single-arm variations to correct asymmetries and reinforce joint control. Even a few weeks of unilateral work can clean up a lopsided press or row and make your bilateral numbers move again.
Control System Features That Cut Scrap Rates
Modern control systems tackle scrap at its source by tightening process window monitoring. Instead of waiting for a full batch to run off-spec, these platforms track real-time deviations in temperature, pressure, and feed rates against tight tolerance bands. When a parameter drifts near the edge, the system either nudges actuators back into range or flags the operator with a clear, actionable alert. This closed-loop adjustment happens fast enough to keep material flowing at spec, which directly reduces the piles of rejected parts at the end of a shift.
Another key feature is the move toward predictive process control. By continuously comparing live sensor data with historical run profiles, the system spots patterns that precede a defect, such as a subtle rise in viscosity or a slight drop in mold cavity pressure. Rather than reacting after a bad part is made, the controller preemptively tweaks dwell time or cooling rates. Over weeks, this learning loop trims the scrap rate further because the same root causes don't keep reappearing across different product lines.
Finally, tighter integration between recipe management and real-time adjustment removes a common source of scrap: operator error. Modern controls store validated parameter sets for each material and tool combination, then automatically load the right profile when a job changes. If a sensor reading falls outside the expected envelope, the system can pause the cycle or suggest a corrective action before the part fully forms. That level of guardrail means fewer mislabeled runs, less rework, and a measurable drop in waste without requiring constant manual oversight.
Material Handling Choices That Speed Up Production
Swapping out manual carts for a well-placed gravity roller conveyor can feel like a small move, but it often removes the hidden pauses where workers wait for parts. The trick is to keep the flow at waist height and avoid transfers that require lifting or reorienting.
Another overlooked lever is the mix of totes and carts at the line. Using modular bins that slide directly into point-of-use racks means restocking happens in seconds, not minutes. Pair that with tuggers or lightweight AGVs for milk runs, and floor traffic drops while the line keeps a steady rhythm.
Proactive Maintenance Habits for Reliable Operation
Operators who stay ahead of breakdowns tend to follow a simple rhythm: they walk the floor at the start of every shift, listen for odd vibrations, and check fluid levels before machines even warm up. It's not glamorous, but catching a frayed belt or a slow leak during a cold inspection saves hours of unplanned downtime later. Small notes in a maintenance log, jotted down without ceremony, often reveal patterns that a dashboard can miss.
Another habit that pays off is scheduling tasks based on actual wear rather than a fixed calendar date. If a pump runs harder in summer, its seals will need attention sooner. Tracking operating hours and load conditions lets the team replace parts when they're genuinely nearing the end of their life, not just because the month changed. This approach cuts costs and avoids unnecessary interventions that can introduce new problems.
Finally, reliable operation depends on sharing what you see. A quick handoff note about an unusual noise or a slightly higher temperature reading gives the next shift a head start. When people treat these observations as part of the job instead of optional extras, equipment failures become less frequent and less severe.
FAQ
Focus on how evenly the oven distributes heat and whether the arm motion supports bi-axial rotation. Minor temperature swings often show up as thin spots or warpage, so machines with tight thermal control and adjustable rotation ratios usually produce more repeatable parts.
A well-designed oven pushes heated air across the mould surface instead of simply surrounding it. Balanced airflow shortens cycle times and prevents scorching on one side, which helps maintain mechanical properties in thick sections.
Multi-arm configurations shine when you run varied mould sizes or need to stagger heating and cooling stages. If your production involves long cycles or frequent mould changes, independent arm control can keep output steady without tying up the whole machine.
Regular checks on burner nozzles, seals, chain tension, and mould clamping areas go a long way. Clearing dust from air intakes and verifying insulation condition also prevents gradual heat loss that quietly raises energy use and cycle times.
Swing diameter determines the largest mould you can rotate without interference. Underestimating it leads to damaged moulds or machine frame stress, while a little extra clearance gives operators room to load parts safely and adapt to new product designs.
Recipe-driven heating and cooling profiles, automatic gas modulation, and remote fault alerts tend to pay off quickly. They reduce operator guesswork and catch small issues before they turn into scrap or unplanned downtime.
Ask for actual gas or electric consumption per kilogram of finished product on a reference mould. Compare burner turndown range, insulation thickness, and whether cooling fans stage automatically instead of running at full speed the whole time.
Quick-release or pneumatic clamping systems reduce the time spent bolting moulds to the spider. Good clamping also keeps parting lines tight during heating, which cuts flash and secondary trimming work.
Conclusion
A shortlist of ten roto moulding machines that consistently deliver superior performance rarely comes down to a single headline feature. The way a frame, arm, and mould mounting system are built has a direct bearing on how precisely walls stay within tolerance months or years after installation. Machines with heavier, stress-relieved structures and well-aligned plates keep rotation smoother, which reduces the slow drift in wall thickness that cheaper units often develop. Heating and cooling cycle adjustments matter just as much: fine-tuning burner output, air flow inside the oven, and the timing of forced-air or water-mist cooling can trim several minutes from each cycle while improving surface finish. When comparing single-arm and multi-arm configurations, the right choice depends on part size and changeover frequency. A single arm may offer more working room for very large tanks, while a multi-arm shuttle or carousel design keeps multiple moulds moving through different stations, making it easier to maintain steady output on small and medium parts.
The best performers in the top ten also share control system traits that help operators catch drifting temperatures, uneven rotation, or pressure drops early, often cutting scrap rates by a noticeable margin without requiring constant manual adjustment. Material handling choices, from vacuum loaders to hopper placement and clean resin transfer lines, reduce downtime between cycles and prevent contamination that weakens parts. Equally important are proactive maintenance habits: daily checks on arm bearings, chain tension, burner nozzles, and thermocouple calibration keep machines from drifting out of spec. Shops that track these small routines tend to get years of consistent wall thickness and fewer emergency repairs. What separates the top ten selections is not a single breakthrough but how well these elements work together, producing a machine that feels predictable under load and keeps delivering tight tolerances without constant babysitting.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com