High Quality Popcorn Production Line: Essential Components for Consistent Output
2026-10-01
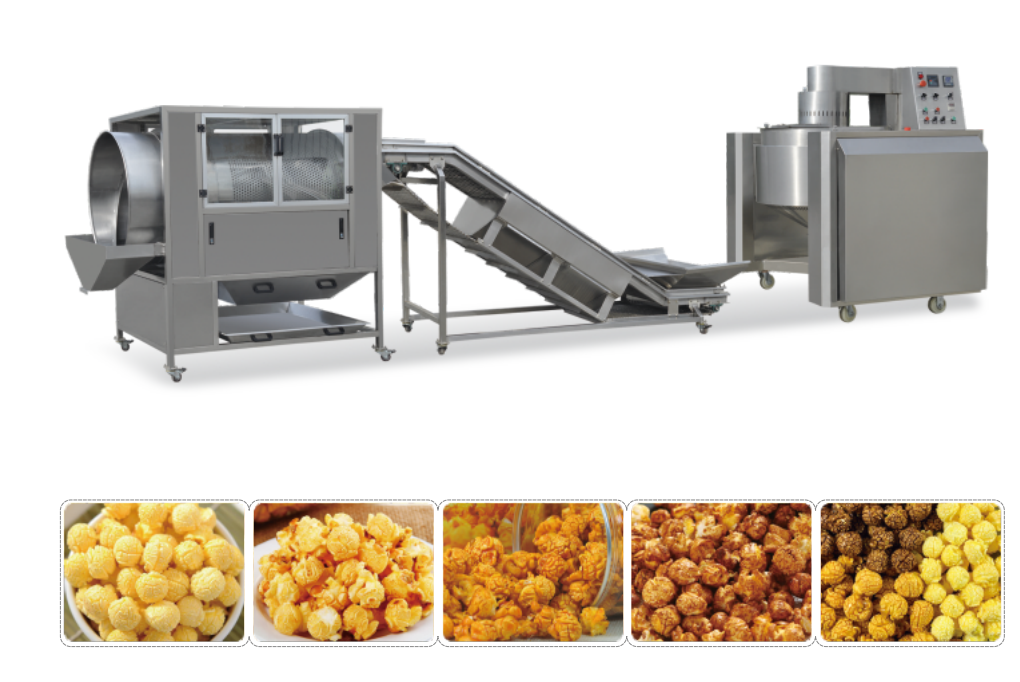
Popcorn seems forgiving until you scale it. At commercial volumes, a few degrees of temperature drift or a poorly matched flavoring drum can turn consistent output into a daily guessing game. This post looks at the essential components of a high-quality popcorn production line—from kernel conditioning to cooling—and how each one affects the final bag. We’ll also highlight how MINGDE designs these modules to work together, so you can spot weak points before they eat into your yield.
Getting the Kettle Right So Every Batch Pops Evenly
Most uneven popping comes down to one overlooked variable: how the kettle heats up before a single kernel goes in. You want a slow, steady climb to around 400°F, not a full-blast blast that scorches the bottom while leaving the top cold. Give the oil a full minute to shimmer and thin out—coconut oil works best because it coats each kernel without smoking out early. Swirl the kettle once or twice as it warms, then toss in three test kernels and wait until all three pop before adding the rest.
Once the full batch is in, keep the kettle moving. A gentle shake every ten seconds prevents the unpopped kernels from settling into hot spots, and it also knocks popped corn away from the heat so it doesn't steam. If you notice a pause longer than three seconds between pops, pull the kettle off the heat for a moment—that small lift can be the difference between a crunchy batch and a bowl full of half-popped rocks.
Why Your Heat Source Changes the Flavor Profile
A gas burner and a lump charcoal fire both register 400°F on a thermometer, but they cook nothing alike. The difference is not just temperature—it is the type of energy transferred and the invisible compounds riding along with it. Charcoal and wood emit radiant heat from glowing embers, which sears surfaces quickly and drives off moisture, while also releasing phenolic compounds, guaiacol, and other volatiles that cling to fat and protein. Gas, by contrast, produces mostly convection heat and water vapor as a combustion byproduct, so the flavor stays cleaner but also more neutral. That is why a steak over charcoal can taste faintly of campfire even before any smoke seasoning is added.
Electric and induction sources shift the profile yet again. They heat the cooking surface directly, with almost no combustion gases or airflow around the food, which means fewer opportunities for browning reactions that rely on dry, high heat and open flame. The Maillard reaction still happens on a hot pan, but the aromatic depth differs because there is no flame licking the edges, no ash, no trace minerals from the fuel. You end up with a purer expression of the ingredient itself—great for delicate fish or eggs, but often lacking the rugged complexity that fire-based methods provide.
Even among wood fuels, the species and moisture content matter more than most people assume. Oak burns hot and steady with a relatively mild smoke, mesquite burns fast and aggressive, and fruit woods like apple or cherry contribute sweeter, softer notes. Green or damp wood smolders and produces creosote-like compounds that can turn bitter. The heat source is not just a utility; it is an ingredient. Choosing charcoal over propane, or oak over hickory, is a deliberate decision that shapes the final aroma, texture, and even the way salt and fat carry flavor on the palate.
Coating and Seasoning Systems That Keep Up With Speed
Modern snack lines run at a pace that would have been unthinkable a decade ago, and the coating drum has to match that tempo without turning product into a mess. A well-designed system meters seasoning and oil in tight, programmable bursts, syncing with the infeed so every piece gets a consistent dusting—not a clumpy avalanche. The difference is in the details: quick-release baffles, drums that angle slightly for better tumbling, and spray bars positioned to coat without drowning the product. Operators can adjust flow rates on the fly, and that flexibility keeps downtime to a minimum when switching from one flavor profile to another.
Speed alone doesn’t win the race, though. The real test is how evenly seasoning clings to every ridge and curve of a chip or extruded snack. Sophisticated systems use a combination of vibration, drum speed, and airstream to toss the product just enough—never so hard that it breaks, never so soft that seasoning pools at the bottom. Some setups even pair a pre-dusting stage with a secondary polish drum, giving the seasoning a chance to set before packaging. That way, the line can run at full throttle and still deliver a bag where the first chip tastes as bold as the last.
Maintenance often gets overlooked until a line goes down, but with high-speed coating systems, easy access is baked into the layout. Removable drums, tool-less nozzle changes, and washdown-ready surfaces mean sanitation crews can get in, clean, and get out without a lengthy teardown. The best designs log sensor data, too—tracking oil temperature, drum RPM, and seasoning flow so any drift from the target shows up before it turns into a quality issue. That kind of foresight keeps a fast line running true, shift after shift.
Moving Popcorn From Kettle to Bag Without Breakage
The worst breakage rarely happens in the popping drum—it happens when you tip a full kettle straight into a narrow bag. The bottom kernels take the weight of everything above them, and any trapped steam makes hot pieces clump together so you end up shaking or crushing the mass just to get it through the opening. A better transfer starts with giving the popcorn somewhere to land that isn't a bag.
As soon as the last kernel finishes popping, tilt the kettle slowly and let the batch fall no more than a few inches onto a wide cooling rack or a shallow sheet pan. Spread it in a single layer if you can. Leave it for about a minute, until visible steam stops rising; that short rest dries the surface and keeps pieces from gluing themselves together. If you season at all, do it now with a very light hand while the corn is still warm, tossing only once or twice.
For bagging, hold a wide-mouth bag on its side and use a scoop or a folded piece of parchment as a slide. Add small amounts at a time, rotating the bag so the kernels settle evenly instead of piling in one spot. Never press down to make room. If the bag is narrow, fill it in three or four small layers, giving it a gentle side-to-side shake between layers, and wait until the popcorn is completely cool before sealing.
Moisture Sensors That Stop the Unpopped Kernel Problem
Most microwave popcorn instructions rely on a fixed cooking time, which almost guarantees a mix of burnt pieces and stubborn unpopped kernels. A moisture sensor changes that by listening to the steam rather than the clock. As kernels pop, they release bursts of moisture, and once that release slows to a trickle, the sensor knows the bag is nearly done and cuts the heat before the remaining kernels have a chance to scorch.
The real advantage is how the sensor adapts to your specific microwave and the particular batch of popcorn. Instead of guessing with a preset timer, the machine reads the actual humidity inside the cooking cavity and reacts in real time. That means fewer hard, unpopped kernels at the bottom of the bag, and more fully expanded, tender pieces overall — without needing to stand by the microwave waiting for the pops to die down.
Quick Clean-in-Place Routines for Flavor Consistency
Flavor drift usually comes down to what's left behind after a cycle, not the recipe itself. A quick CIP routine works if it targets the exact residue your product leaves—sugars, oils, or acids—rather than treating every line the same way. Start by draining the system fully while it's still warm; letting product cool in place makes even a fast rinse slower and less effective.
Keep the alkali wash short but hot, around 160–170°F, and don't dilute beyond the chemical supplier's range just to save minutes. Run it through all spray balls, dead legs, and sample ports for at least five minutes of true contact time. Follow immediately with an acid rinse to neutralize and pull mineral films, then flush with cold water until the outlet runs clear and the conductivity flatlines.
Verification doesn't have to be complicated. Sniff the drain, rub a clean white cloth inside a valve or gasket, and check the final rinse water pH. If anything smells like the previous batch, repeat the rinse before you even think about the next product. Log your times and temperatures in a simple notebook; flavor consistency is easier to keep when you can spot a slow drift in your CIP data before it shows up in a tank.
FAQ
The core difference usually comes down to the popping chamber design and how precisely the heat source is controlled. Reliable lines keep kernels moving evenly across the hot surface, preventing scorching in one spot while leaving others unpopped. A well-engineered agitator with adjustable speed, combined with temperature sensors that react within seconds rather than minutes, makes far more difference than most people expect. Lines that skip these refinements tend to suffer from clogging around the discharge chute because partially popped kernels or hulls pile up instead of being pushed out smoothly.
The popping kettle's temperature profile and the way residual heat is managed. A kettle that holds heat too long after the burners cycle off will start to shrink and toughen the popped corn, while one that cools too quickly leaves a slightly chewy center. In practice, this means choosing a kettle with enough thermal mass to stay stable during load changes but also with an exhaust or cooling jacket that quickly drops below popping temperature once the batch is done. Operators who learn to read the flake size and listen for the popping rate can make small adjustments that keep the output uniform.
A two-stage approach works best: apply oil or a binding agent first while the popcorn is still warm and tumbling, then introduce dry seasoning in a rotating drum with baffles that gently fold the product. The oil needs to be atomized, not dripped, so it spreads into a thin film rather than pooling. After seasoning, run the conveyor for a short drying pass or use a vibrating screen to knock off any loose powder before packaging. Regular wiping of the drum interior and checking that the spray nozzles aren't partially blocked will prevent the sticky buildup that eventually causes conveyor belts to slip.
Ignoring the small wear points around the popping chamber discharge door and the kettle seal. A slight leak there lets unpopped kernels and hulls accumulate in places they shouldn't, which leads to jams that shut down the whole line. Another overlooked item is the air filtration on the cooling tunnel: when filters clog, the cooling air slows down, condensation forms, and the popcorn picks up moisture again before bagging. Checking and replacing those filters on a schedule, along with greasing the drive chains on the seasoning drum, prevents the majority of sudden stops.
It genuinely changes the texture. A flat, thin-bottom kettle tends to produce smaller, denser flakes because the heat is applied too quickly to the kernel surface. A thicker, curved-bottom kettle with multiple heat zones allows the kernel to heat more gradually, so the starch gelatinizes fully before the hull ruptures, giving a larger, crispier, and more delicate flake. The difference is noticeable in side-by-side tests, especially with butterfly or mushroom hybrids. So it's not marketing—it's a combination of heat distribution, kettle shape, and how quickly the popped corn is removed from the hot zone.
The problem is usually not the incoming corn moisture but what happens to it during holding and transfer. If the raw kernels are stored in a silo that gets hot during the day and cold at night, condensation can form inside and raise the surface moisture just enough to cause wet, chewy pops. The same issue occurs when the conveyor from the silo to the kettle passes through a humid room. Solving it often means installing a small dehumidifier in the kernel hopper or simply keeping the transfer path as short and sealed as possible. Monitoring the moisture at the kettle inlet, not just at receiving, catches these shifts early.
After popping, the residual steam inside each flake needs to escape before the popcorn is sealed in packaging. A cooling stage with dry, moving air pulls that moisture away from the surface and lets the flake set into its final crisp structure. Without this step, the trapped steam condenses inside the bag, making the popcorn tough and causing seasonings to clump. Lines that use a perforated conveyor with forced air at around room temperature, but with low humidity, consistently produce bags that stay crisp much longer than lines that package warm popcorn.
Conclusion
A truly consistent popcorn line starts with the kettle, where even heat distribution and precise agitation keep every kernel popping at the same rate. Pairing that with the right heat source—whether direct flame, electric, or hot air—shifts the flavor profile subtly, from toasted nuttiness to clean, buttery sweetness. Once popped, the coating and seasoning stage must keep pace with high-speed output without clumping or uneven coverage. Moving the finished popcorn from kettle to bag demands gentle conveyors and drop heights tuned to minimize breakage, so the final product looks as good as it tastes.
Moisture sensors play a quiet but critical role, catching low-moisture kernels before they become hard, unpopped surprises in the bag. Finally, quick clean-in-place routines keep flavor consistent from batch to batch, preventing stale oil or seasoning buildup from muddying the taste. When all these components work together, the line delivers uniform texture, reliable flavor, and a crunchy, intact product that keeps customers coming back.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/